Recent innovations in large capacity refrigerated centrifuge wholesale technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders large capacity refrigerated centrifuge wholesale equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.

From research in the laboratory to large-scale production, large capacity refrigerated centrifuge wholesale devices have a place in processes requiring precision and efficiency. They purify reaction mixtures and solvents in chemical production. Hospitals rely on large capacity refrigerated centrifuge wholesale for the testing of patients and therapeutic treatment. In farming, large capacity refrigerated centrifuge wholesale are used to study plant biology and develop fertilizer formulations. In brewing and winery operations, they provide consistency within products by filtering out impurities. Even environmental engineers rely on large capacity refrigerated centrifuge wholesale to filter sediment as well as identify contaminants. Such wide-ranging functionality demonstrates its vital position in contemporary technology and applied sciences.
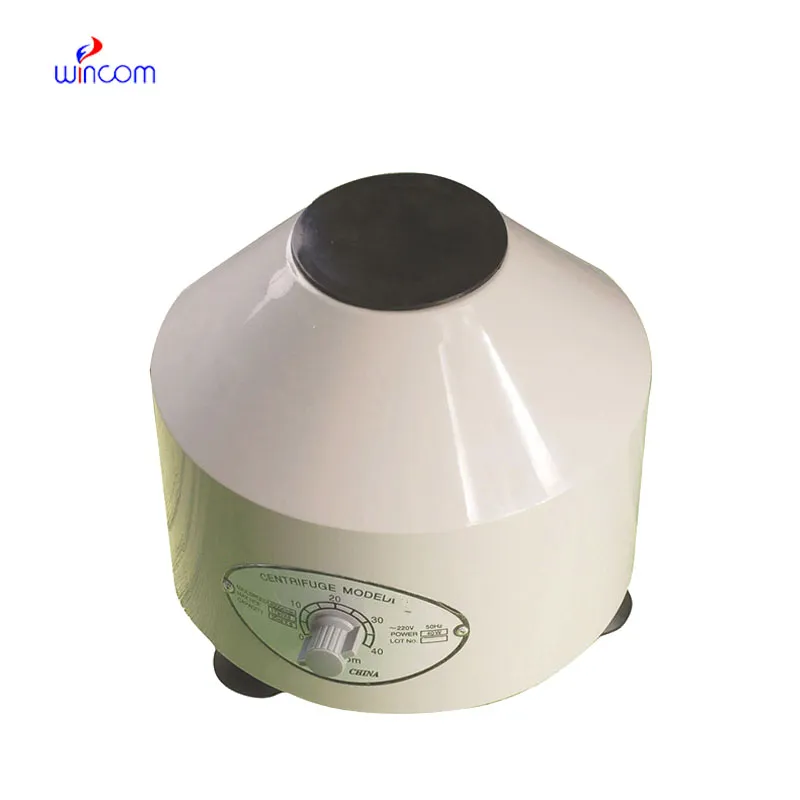
Future trends show that large capacity refrigerated centrifuge wholesale will become more intelligent, miniaturized, and green. Researchers envision systems capable of learning for themselves and optimizing their performance from previous data results. Integration within digital laboratory workflows will render operations, from sample entry to data reporting, more seamless. Increased automation will free researchers from manual monitoring, allowing more focus on analysis. In industrial processes, large capacity refrigerated centrifuge wholesale will have a role in cleaner production through the reduction of waste and energy usage. It is a step toward smarter scientific instrumentation that adapts to the challenges of technology.
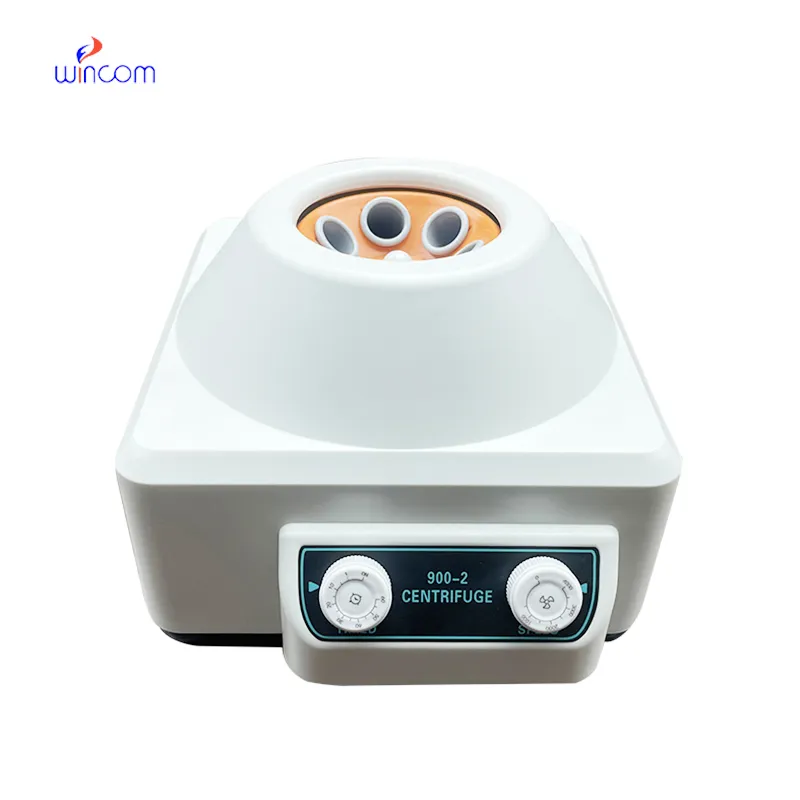
Routine maintenance of large capacity refrigerated centrifuge wholesale begins with frequent cleaning and careful handling. Before each run, users should confirm that there are properly sealed, loaded tubes to prevent imbalance. The rotor, buckets, and seals should be washed gently and dried with air after each session. Periodic calibration checks ensure precise speed and temperature measurement. Rotor overloading is to be prevented since it will reduce motor life. With monitoring each maintenance cycle and adhering to safety protocols, laboratories can extend the functional life of large capacity refrigerated centrifuge wholesale while ensuring precise performance.
Through controlled rotation, a large capacity refrigerated centrifuge wholesale produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most large capacity refrigerated centrifuge wholesale today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the large capacity refrigerated centrifuge wholesale a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
Could you please provide more information about your microscope range? I’d like to know the magnif...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko