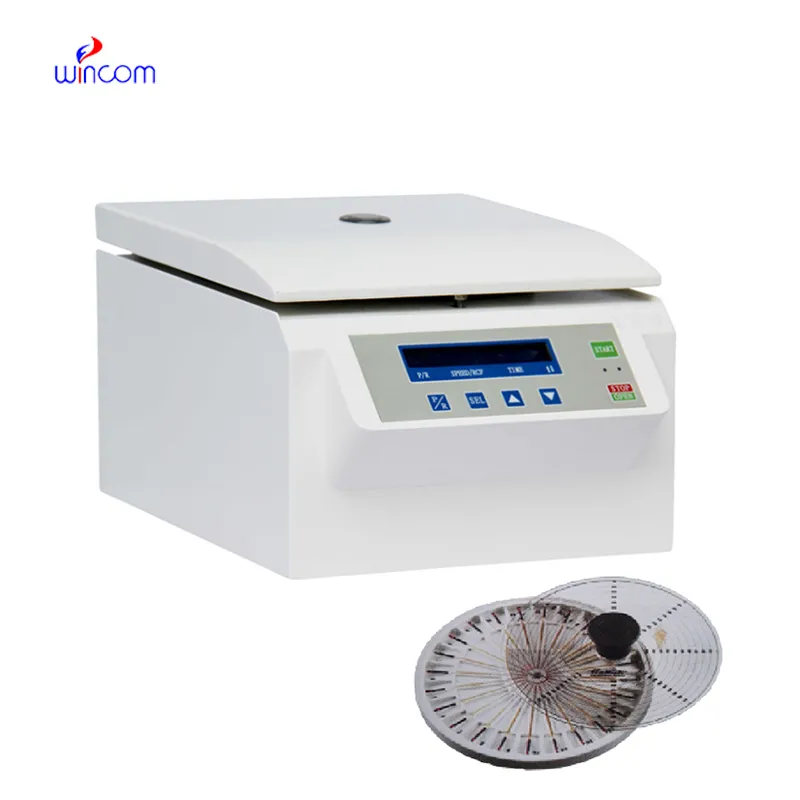
Recent innovations in super large capacity refrigerated centrifuge technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders super large capacity refrigerated centrifuge equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.

super large capacity refrigerated centrifuge technology is a principal component in diverse manufacturing processes. In wastewater treatment, super large capacity refrigerated centrifuge assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, super large capacity refrigerated centrifuge facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, super large capacity refrigerated centrifuge continues to support industries seeking consistency, purity, and scalability.
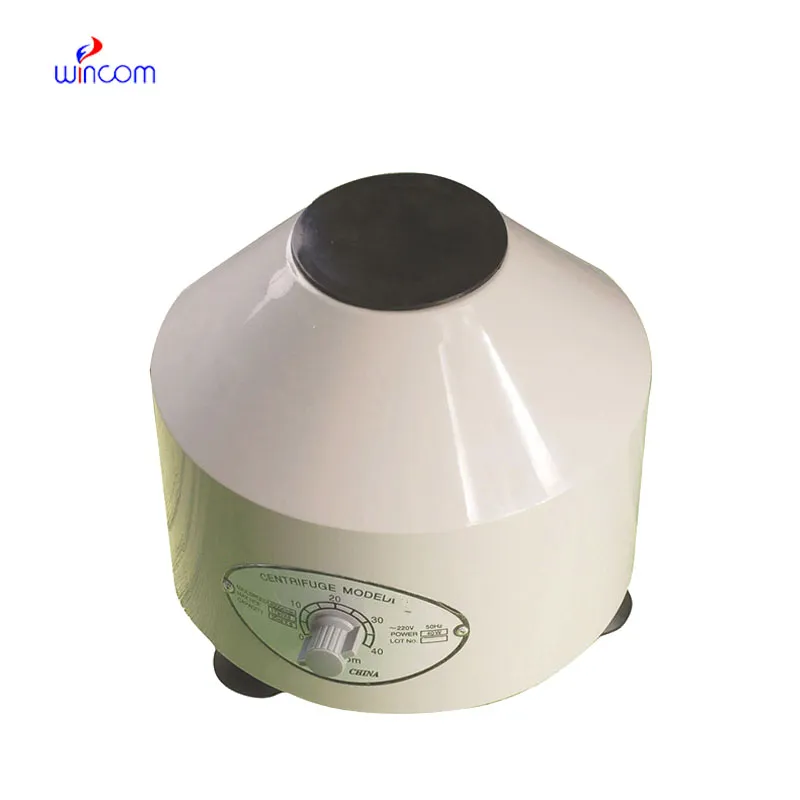
The super large capacity refrigerated centrifuge technology future lies in automation, digital control, and green engineering integration. Future models will include AI algorithms for speed, balance, and separation efficiency automatic optimization. Energy-efficient motors and recycled materials will reduce environmental impact, following international sustainability goals. Cloud connectivity will allow for remote monitoring and predictive maintenance, with less downtime. In laboratories, super large capacity refrigerated centrifuge will be completely compatible with smart data systems for real-time reporting and process validation. These innovations promise greater accuracy, reliability, and versatility for research and industrial use.
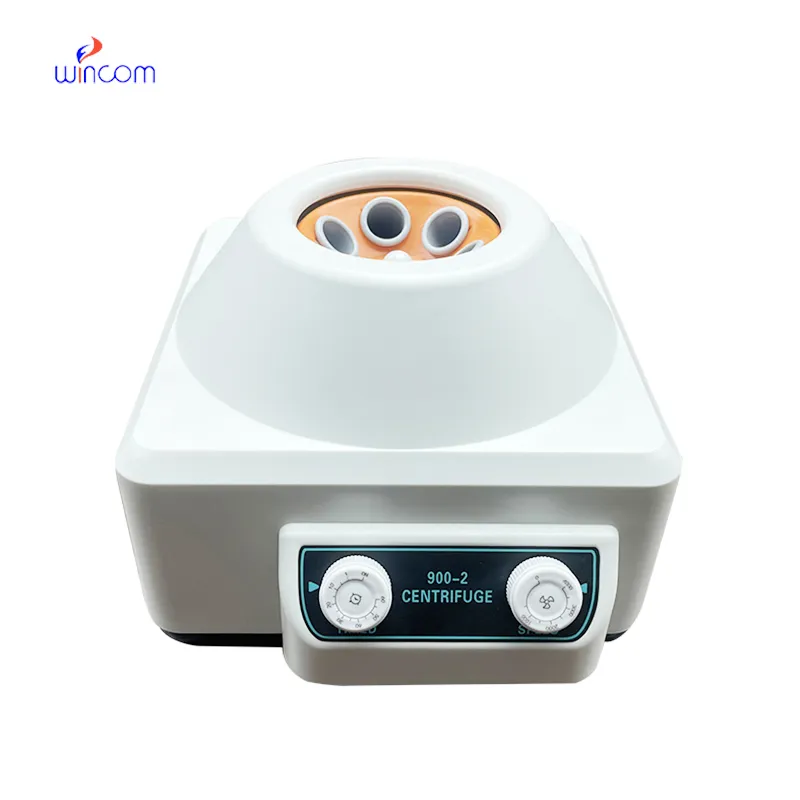
For long-term efficiency, super large capacity refrigerated centrifuge must be maintained with thorough attention to detail of operation. Every rotor and adapter must be checked for integrity before sample loading. After every cycle, the apparatus needs to be washed with neutral detergents and dried thoroughly. Vibration and mechanical stress are prevented by regular tests of balance. Seals and filters need to be replaced according to service schedules. Dust deposition is prevented by keeping the instrument in a covering when not used. If super large capacity refrigerated centrifuge apparatus is cared for according to disciplined procedure, equipment will give consistent high-performance performance year in year out.
super large capacity refrigerated centrifuge revolutionized laboratory and industry processes of substance separation forever. By speeding up the sample at high speed, they produce an immense force that separates mixtures based on particle density. This is the mechanism that enables efficient extraction of biological compounds, chemicals, and nanoparticles. Laboratories apply super large capacity refrigerated centrifuge for analysis, purification, and research. In industry, they enable the refining of oil and food quality analysis. Small tabletop units and industrial units both use the same fundamental principle—precision with rotational energy and controlled acceleration.
Q: What are the main components of a centrifuge? A: Key components include the rotor, motor, control panel, safety lid, and chamber, each working together to achieve precise separation. Q: How can I verify that a centrifuge is functioning correctly? A: Check that the machine runs smoothly without any unusual vibrations or noises, check the speed accuracy and evaluate the results to ensure consistent separation. Q: Is it safe to open a centrifuge immediately after use? A: No, the device should come to a complete stop before opening to avoid injury or sample disruption. Q: How should a centrifuge be stored when not in use? A:Store it unplugged, covered, and in a dry, dust-free environment to protect internal components from moisture and corrosion. Q: Can centrifuge operation be automated? A: Yes, modern models include programmable controls and digital interfaces that allow automated speed, time, and temperature settings.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko